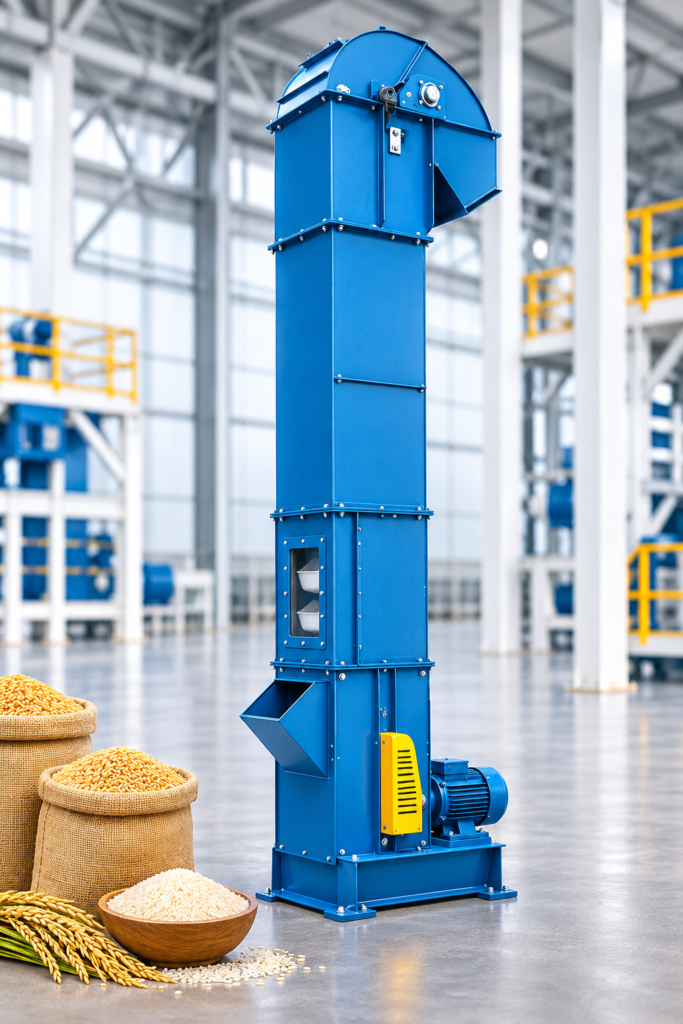
Gillko Engineering’s Bucket Elevator is designed to transport grains and other suitable bulk materials vertically between different processing levels. Its bucket-based conveying mechanism lifts materials efficiently while helping minimize spillage and reduce manual handling.
Ideal for rice mills, grain processing plants, warehouses, and agricultural facilities, the Bucket Elevator supports smooth material movement between cleaning, grading, storage, and milling equipment. Its space-saving vertical design makes it a practical solution for facilities looking to improve material handling efficiency.
The Bucket Elevator is an essential material handling machine for transporting grains vertically in industrial processing facilities. It uses a series of buckets attached to a moving belt or chain to lift materials from a lower feeding point to a higher discharge point.
Designed to support continuous conveying operations, the machine helps maintain a smooth flow of materials throughout the production process. Its vertical configuration makes efficient use of available floor space, while its enclosed conveying arrangement helps reduce material loss during transportation.
Efficient Vertical Conveying: Moves grains between different processing levels.
Low Spillage: Helps minimize material loss during lifting and discharge.
Space-Saving Design: Supports vertical transportation with a compact footprint.
Reliable Operation: Designed for regular use in grain processing facilities.
Multiple Size Options: Available in different sizes to suit varying operational requirements.
Power Options: Motor configurations are available according to the selected model and lifting height.
| Parameter | Available Options |
|---|---|
| Size | 6, 8, 10, 12, 14 inches |
| Power (up to 30 ft.) | 1 HP, 1.5 HP, 3 HP, 3 HP, 5 HP |
Specifications are based on the supplied product image. Confirm the exact motor power for each size with Gillko Engineering before publishing.
The Bucket Elevator is suitable for:
Rice mills and grain processing plants
Paddy and grain cleaning facilities
Flour and agricultural processing units
Grain storage and handling facilities
Industrial material conveying systems
Improves the efficiency of vertical material transportation.
Helps reduce grain spillage during conveying.
Supports smooth material flow between processing machines.
Makes better use of available factory floor space.
Reduces the need for manual material lifting.
Gillko Engineering provides grain processing and material handling equipment designed for industrial requirements. Our Bucket Elevator offers a practical solution for vertical grain transportation, helping businesses streamline operations and maintain an efficient material flow.
Discover dependable grain processing and material handling machinery designed to support your business operations.
Reliable machinery solutions for rice mills, grain handling, and seed processing. We are committed to quality engineering, efficient operations, and customer satisfaction.
+91 9989776545
gillkoengineering@outlook.com
Shanti Kunj City, Chhanchhan Paeri, Old Dhamtari Road, RAIPUR (C.G.)
© 2026 Gillko Engineering. All Rights Reserved. Designed by Navel Studio