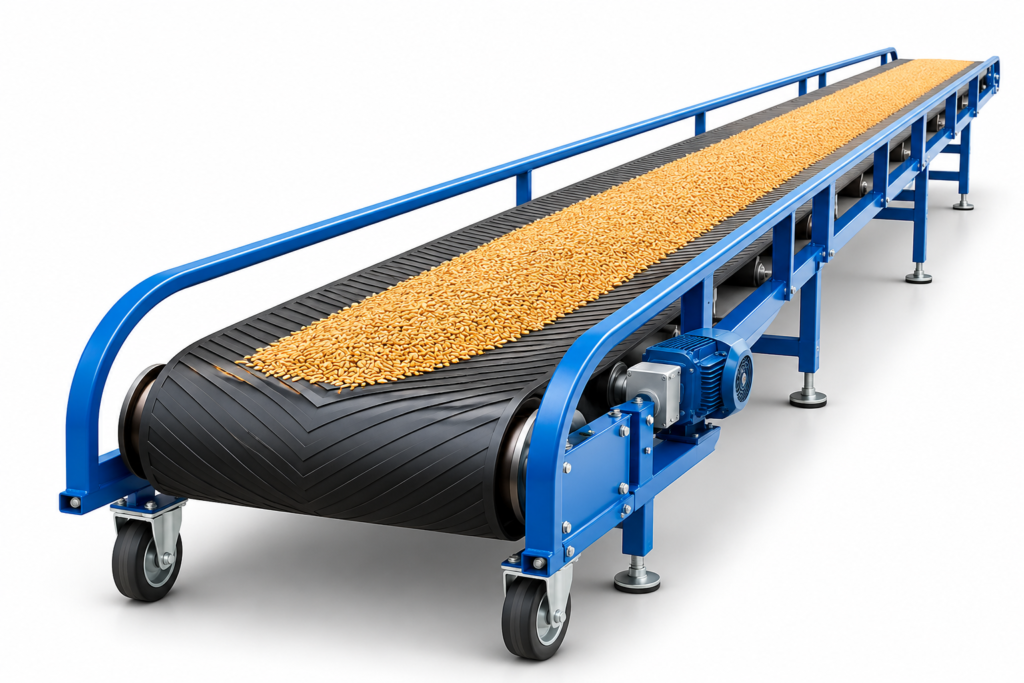
Gillko Engineering’s Belt Conveyors are designed to transport bulk grains efficiently within rice mills, storage facilities, and grain processing plants. Their continuous belt system ensures smooth material movement across horizontal and inclined surfaces, helping reduce manual handling and improve operational efficiency.
Gillko Engineering’s Belt Conveyors are designed to transport bulk materials such as grains efficiently within grain mills and industrial facilities. Their continuous belt system ensures smooth, reliable material movement across horizontal and slightly inclined surfaces.
Efficient Material Handling: Moves large quantities of grain with ease.
Continuous Operation: Supports smooth and consistent material flow.
Versatile Applications: Suitable for grain mills, storage silos, and processing plants.
Reliable Performance: Designed for dependable industrial use.
Flexible Installation: Can be adapted to different material handling layouts.
Belt Conveyors are ideal for rice mills, grain processing facilities, warehouses, storage silos, and truck loading operations where efficient bulk material transportation is required.
Improves material handling efficiency.
Reduces manual labor and handling time.
Supports smooth movement of bulk grains.
Helps streamline industrial operations.
Gillko Engineering provides practical and reliable conveyor solutions designed to meet diverse grain handling requirements. Our Belt Conveyors help businesses improve workflow efficiency and maintain consistent material movement.
Discover dependable grain processing and material handling machinery designed to support your business operations.
Reliable machinery solutions for rice mills, grain handling, and seed processing. We are committed to quality engineering, efficient operations, and customer satisfaction.
+91 9989776545
gillkoengineering@outlook.com
Shanti Kunj City, Chhanchhan Paeri, Old Dhamtari Road, RAIPUR (C.G.)
© 2026 Gillko Engineering. All Rights Reserved. Designed by Navel Studio